A coordinate measuring machine asks one simple question: where is this feature, in X, Y and Z, and is it still there after the cutter has gone? That question is the whole discipline of precision measurement, and a garage shop answers it every time it squares a vise, spots a hole or checks a shaft against its drawing.
The best coordinate measuring tools for home machinists are the ones that turn that question into a repeatable step. They fall into three groups: a probe or edge finder that finds the X and Y position, a height gauge or height setting probe that fixes the Z number, and a reference surface that both are read against. Pick one from each group and you have a working coordinate setup for a fraction of what a real CMM costs.
What follows is 2026‘s working shortlist: ten coordinate measuring tools we looked at side by side, the honest limits of each, and a workflow for putting them together. Every accuracy figure quoted here comes from the manufacturer specification for that exact model, and we flag the cases where reviewers report something different from the datasheet. If you are still outfitting a first bench, the [workflow section](#building-a-home-shop-coordinate-measurement-workflow) near the end is the fastest route.
We also spend a lot of time on our other hobby-bench guides, from picking a [turntable for home listening](https://www.theclassicalshop.net/best-turntables-for-home/) to balancing [cartridge alignment on a stylus](https://www.theclassicalshop.net/best-cartridge-alignment-tools-for-turntables/) – the same slow, evidence-first approach applies to a ten-thousandth of an inch decision as it does to a tonearm.
Table of Contents
Top 3 Picks for Best Coordinate Measuring Tools (October 2026)
SainSmart CNC Z-Axis Tool Setting Probe
- Automatic tool height checks
- Works with Mach3 and Grbl
- Light 0.03 kg body


Brown and Sharpe Edge Finder
- Plus or minus 0.0005 inch
- 0.200 inch tip
- Standard 3/8 inch shank
Our first pick is the probe most home machinists meet first, because it removes the paper-slip method from the first afternoon of CNC work. The two edge finders behind it are the manual answer to the same job, and between the three you can locate a workpiece on any mill, manual or CNC.
All 10 Best Coordinate Measuring Tools at a Glance in 2026
| Product | Specifications | Action |
|---|---|---|
| SainSmart CNC Router Z-Axis Tool Setting Touch Probe |
|
Check Latest Price |
 PGFUN DIY CNC Touch Probe XYZ 3D Digitizing Edge Finder |
|
Check Latest Price |
 iGaging Digital Electronic Height Gauge 6 Inch |
|
Check Latest Price |
 Shars 12 Inch Dial Height Gage 303-4410 |
|
Check Latest Price |
 Diydeg CNC 3D Finder Universal 3D Sensor Probe |
|
Check Latest Price |
 YIDOFENG MF60 3D Touch Probe Edge Finder |
|
Check Latest Price |
 Starrett Electronic Height Gage 0-6 Inch |
|
Check Latest Price |
 Mxmoonfree 12 Inch Digital Height Gauge |
|
Check Latest Price |
| Starrett 827B Edge Finder |
|
Check Latest Price |
| Brown and Sharpe Standard Edge Finder |
|
Check Latest Price |
Read that table as three families, not ten competitors. Four entries are CNC probes that find a coordinate under machine control, three are height gauges that read a Z height by hand, and two are mechanical edge finders that centre a part by feel.
What a Coordinate Measuring Machine Does and What a Home Shop Uses Instead
A coordinate measuring machine is a three-axis bridge or gantry that carries a touch probe, moves it to a commanded X, Y and Z position, waits for the probe to trigger, and records the point. It reports the result as a set of coordinates, compares those coordinates to a nominal model, and prints a deviation report.
That breaks into four jobs: locating a point in X, Y and Z; capturing the size and shape of a feature; repeating the check over many parts; and writing the numbers down somewhere other than a scrap of paper. A home shop does the first three constantly and mostly skips the fourth.
There is also a family of vision measuring machines, which use a camera and software to read an entire part at once rather than touching it. The practical difference for a garage is cost and footprint – a CMM needs levelled granite, a controlled room and an operator who understands datum establishment, which puts it firmly in the small-business category rather than the home-shop one.
The mapping matters more than the brand names, so here is the shortcut. For X and Y location on a manual mill, the tool is an edge finder read against the knee or table graduations. For X, Y and Z under machine control, it is a 3-axis touch probe that reports a trigger point back to the controller. For Z height on a bench or a machine table, it is a height gauge with a movable head. For the reference that all three read against, it is a flat, stiff, clean surface.
One more job, deviation and alignment measurement, is the one a CMM does far better than hand tools because it holds a stylus on a known point and swings it through an arc. In a home shop that job belongs to a dial test indicator on a magnetic base, and it is the natural next purchase after any of the tools above.
So the honest answer to “which coordinate measuring tools do I need” is: one thing to find the part, one thing to read the height, and one flat surface that neither of them is allowed to move.
1. SainSmart CNC Router Z-Axis Tool Setting Touch Probe – Best for First CNC Tool Height Checks
SainSmart CNC Router Z-Axis Tool Setting Touch Probe, Compatible with Grbl/Mach 3
Z-axis tool height probe
0.98 inch and up range
Mach3 and Grbl control
0.03 kg ABS and aluminum
Pros
- Removes the paper slip method for tool height setting
- Works with Mach3 and Grblcontrol software
- Automatic check function returns the machine to a defined position
- Lightest tool in the roundup at 0.03 kg
- Largest review base here with 1152 ratings
Cons
- ABS plastic and aluminum build is not as durable as an all-metal stylus
- Z-axis only so it does nothing for X and Y location
- Sized for the 3018 series hobby routers it was designed around
The first thing this probe does is remove a bad habit. The paper method – sliding a slip of paper under the bit until it just grabs – is fast and it is wrong, because it measures paper thickness and squareness rather than the actual tip of the cutter. A probe that fires a signal at a repeatable trigger point gives you a number the machine can store and reuse every time the tool comes back into the work.
Setup is the part that surprises people. You mount it somewhere fixed on the Z axis, connect it to the breakout board, and tell your control software that this input is a tool setter. From then on, the auto-check routine drives the axis down until the probe triggers and the controller records the Z offset, all from a mouse click.
Weighing 0.03 kg and measuring 1.18 by 1.18 by 0.55 inches, it adds almost nothing to a moving gantry and will not noticeably slow a small router. The measuring range of 0.98 inch and upward is not a limitation in normal use, because the probe only has to span the gap between a tool tip and a fixed reference point during the descent.
Material choice is the honest trade. The body is acrylonitrile butadiene styrene with an aluminum frame, and reviewers are clear that it will not survive the same abuse as a metal stylus. On a hobby router where the tool is covered by an enclosure, that is an acceptable deal. On a machine with a coolant hose pointed at the frame, it is a part you will eventually replace.
With 1152 ratings averaging 4.5 stars, this is by far the most widely used tool in the roundup, and that volume is itself evidence. When an inexpensive part has thousands of owners, failure modes show up in the reviews instead of hiding, and the recurring comment is that the auto-check function simply works.
How it fits into a coordinate workflow
This probe covers the Z coordinate only, and it covers it in a way nothing else on the list does: automatically, repeatably, and without a human reading a dial. On a CNC router the X and Y origin is usually established by eye or by a manual edge finder, so the pairing is a manual edge finder for XY and this probe for Z. Once both are working, the tool length offset set here survives power cycles and gets called on every job.
It is also the only tool here that stores measurement data automatically. A height gauge reading has to be written down by hand; a probe reading lands in the controller log alongside the job. For a shop that runs the same part repeatedly, that record is worth more than the reading itself.
Where it falls short
Three limits are worth stating plainly. It measures no X or Y, so it cannot be used to find a workpiece edge or centre a bore. It is built for small hobby routers and light gantries, where the probe has to move quickly and reset, not for a heavy machine that would need a rigid metal mount. And the light-plastic construction is the first thing to inspect after a year of use, particularly around the cable entry.
If you run a Bridgeport-style manual mill and no CNC, this probe does nothing for you. Look at the Starrett and Brown and Sharpe edge finders later in this guide instead, and at a height gauge for the Z number.
2. PGFUN DIY CNC Touch Probe XYZ 3D Digitizing Edge Finder – Best for Full XYZ Probing
PGFUN DIY CNC Touch Probe XYZ Axis 3D Digitizing Edge Finder 3-Coordinate Measuring Sensor Kit with 6 mm Shank & 2.0 mm Tungsten Steel Ball Tip
XYZ 3-coordinate probe
0.01 mm repeatability
DC5-24V NPN-NO
6 mm shank, 2.0 mm tungsten ball
Pros
- Reports position in all three axes rather than Z alone
- 0.01 mm repeatability suits fine feed rates
- Works with GRBL and MACH3 or Mach4 as well as LinuxCNC
- Black anodized body with a flat anti-roll face
- Can be reconfigured as a tool setter with a base and flat tip
Cons
- DIY grade product not intended for industrial duty
- Needs a breakout board with a three-port probe input
- 1.6N Z-axis trigger force sets your tool setter sensitivity floor
This is the closest thing to a coordinate measuring machine that fits inside a hobby CNC, and the difference from the probe above is the whole point of it. Where a Z-axis tool setter fires once at a single point, a three-axis probe reports a trigger in any direction, which means the machine can find an edge, touch a corner, or follow a profile without you touching a handwheel.
The electronics do the modern half of the job. A DC 5-24V supply with NPN normally-open wiring feeds a single signal back to the controller, and because the trigger is a discrete event rather than an analogue value, the position is simply wherever the machine stopped. That is why the accuracy claim of 0.01 mm, or about 0.0004 inch, is quoted as repeatability rather than absolute accuracy.
Control software coverage is unusually wide for a hobby part. GRBL, MACH3, Mach4, Dynamotion, LinuxCNC, UCCNC and Centroid CNC are all listed, which means it will drop into most control boards people actually own. The 6 mm shank is a common holder diameter, and the 2.0 mm tungsten steel ball tip is the part that touches the workpiece.
Sensing distance is 4 mm with over-travel protection of plus or minus 4 mm in XY and 2 mm in Z. The trigger force figures matter more than they look: 0.5 to 0.82N on the XY axes and 1.6N on Z, which is firm enough to reject vibration but light enough not to deflect a thin part.
Owners also like the flat anti-roll design on the body, which keeps the probe from rotating in the holder and giving a false repeat trigger. It matters more than it sounds, because a probe that rolls a fraction of a degree between passes will report a different edge every time.
Where it earns its place
The real value is digitizing. A three-axis probe plus a controller that supports probing lets you record actual point data and export it, which turns loose machining into something you can measure rather than guess. You can find a true hole centre, check whether a milled pocket is square to the table, or locate a workholding fixture repeatably on every setup.
Because the repeatability is 0.01 mm, the natural home for it is fine small-diameter end mills in aluminium, brass or plastics where a light trigger will not mark the work. Pair it with a 1-2-3 block or a known reference so every setup starts from the same place.
Where it falls short
The honest limitation is that this is a hobby part. It is not built for continuous industrial duty, and the 42 ratings tell you the long-term data set simply does not exist yet. The wiring is not trivial either – a breakout board with a three-port probe input is a prerequisite, and if your board only has a single probe channel, this will not work without extra hardware.
The 1.6N Z trigger force also sets a floor: a tool setter built around it has to be more sensitive than that, or it will push through a light probe instead of registering it. Plan the electronics before you buy the probe, not after.
3. iGaging Digital Electronic Height Gauge 6 Inch – Best Budget Z-Axis Coordinate Gauge
iGaging Digital Electronic Height Gauge with Magnetic Base, 6 Inch
6 inch capacity
0.0005 inch accuracy
Magnetic base
Fraction, decimal and mm readout
Pros
- Accurate to 0.0005 inch on a magnetic base
- Reads fractional inches
- decimals and millimetres
- Flat-sided gauge block lies on its side for setup work
- CR2 batteries included in the box
Cons
- No fine adjustment knob for thousandths work
- Drains batteries during long storage
- CR2 coin cells are awkward to source in a hurry
A height gauge is the closest hand tool to the Z axis of a coordinate measuring machine. You set the head against a datum surface, zero it, slide the carriage down, and read a height directly – no interpolation, no estimating which line on the vernier is correct, and no dependence on your eyesight under a bench lamp.
This one is 6 inches of capacity with an accuracy figure of 0.0005 inch, and the accuracy is stated as a resolution plus a real accuracy claim rather than resolution alone. That distinction matters: a display that can show 0.0005 inch is not the same as a tool that is correct to 0.0005 inch anywhere on the scale.
The display is the reason many hobby machinists end up owning one. It reads fractional inches, decimal inches and millimetres, so you can work to fractions without doing arithmetic and switch to metric for imported drawings. For a beginner, removing the learning curve of a vernier scale is worth more than the last digit of accuracy.
The flat-sided gauge block is the detail experienced users mention most. Most height gauges need to sit upright on a base; this one can roll onto its side, which means you can drop it straight onto a mill table and read a fence-to-bit dimension or a tool height without moving it into a fixture first.
The magnetic base is what keeps it honest. A height gauge on a wobbly reference plate measures the wobble, and the weight and magnet are there to stop that happening on a surface plate or a machine table.
How to get a clean reading from it
Set the gauge on the datum first, close the jaws gently on the surface, and zero. Then slide the head to the feature and read. The single biggest source of error is touching the workpiece hard enough to rock it, so close the jaws until they just touch and stop.
For layout work, treat the 0.0005 inch figure as the practical limit of what the head can repeat reliably, not as a promise on every part of the scale. A tool that is correct at the base and slightly off at full extension will still get you layout marks that a cutter can follow.
Where it falls short
The missing fine adjustment knob is the complaint that appears most often. Without a thumb wheel to bring the carriage down gently, getting to a specific thousandth means sliding the head and stopping by feel, and reviewers describe it as difficult to make fine adjustments at that level.
Battery behaviour is the second issue. The gauge is specified for two CR2 cells, which are included, but owners report it drawing them down while sitting in storage, and coin cells are not the batteries anyone keeps around the house. A fresh set is a small job, but it is a Saturday-morning job rather than a mid-project one.
At 2.05 pounds it is also genuinely heavy for a 6 inch gauge, which is fine on a bench but tiring to carry between machines all day.
4. Shars 12 Inch Dial Height Gage 303-4410 – Best for Large Workpiece Layout
Shars 12″ Dial Height Gage 303-4410 R]
12 inch range
0.001 inch graduation
Plus or minus 0.0016 inch accuracy
Hardened steel rack
Pros
- 12 inch of travel covers large plates and castings
- Fine adjustment thumb roll makes slow positioning easy
- Carbide tipped scriber and scriber clamp included
- Hardened stainless steel rack resists deflection
- Shock-proof white dial face is easy to read under shop lighting
Cons
- Dial format needs interpretation rather than a direct numeric readout
- Graduation of 0.001 inch is coarser than the digital gauges here
- Weighs 6.91 pounds making it a bench tool rather than a portable one
This is a mechanical height gauge, and that is the important thing to understand before you buy one. A dial height gauge reads like a clock: a large hand on a fine scale and a smaller counter hand that tracks whole tenths of an inch. The result is continuous, analogue and completely battery-free, at the cost of requiring you to read two scales at once.
For layout on a big plate or a casting, that is an advantage. The 12 inch of travel is the widest in this roundup for a bench gauge, the rack is hardened stainless steel so it will not rack under a hard shove, and the shock-proof white dial face with 0.1 inch per revolution on the counter is legible at arm’s length on a bench.
Accuracy is stated as plus or minus 0.0016 inch with 0.001 inch graduation, so the graduation is finer than the accuracy figure. That is the honest way to publish it: you can read to a thousandth, and the tool holds a consistent few thousandths over 12 inches of travel.
The fine adjustment thumb roll is the feature that separates a usable height gauge from a frustrating one. It lets you bring the head down slowly and stop exactly on a mark, which is what you need when the scriber is cutting layout lines rather than checking a finished part. Shars also includes a carbide tipped scriber and the clamp that holds it, which is the part most people forget to buy separately.
Coming in 6, 8 and 12 inch variants means the same gauge design scales to the work, and the 6 inch version covers most garage jobs. Owners also point out that the traditional dial format has its fans precisely because there is no battery to die in the middle of a layout session.
When a dial height gauge is the right answer
Reach for it when the job is setup rather than inspection. Squaring a plate, scribing a bolt pattern, copying a hole location from a model, or setting a fence height all benefit from a continuous reading and a fine thumb roll. None of them needs a digital display, and all of them benefit from not having a battery.
The carbide scriber is the reason to treat it as a layout instrument rather than a measuring one. A hard scriber tip marks steel without drifting, where a pencil or a scribe in a plastic holder follows the hand. If you lay out from a model or transfer coordinates by hand, that tip will earn its keep quickly.
Where it falls short
If you are new to reading gauges, this is a harder instrument than a digital one. Two hands, a 0.001 inch dial and a 0.1 inch counter is a lot to parse while wearing safety glasses, and beginners consistently report stalling on it.
The accuracy figure of plus or minus 0.0016 inch also rules it out for the last stage of inspection on tight work. A digital height gauge that reads 0.0005 inch and costs less is the better verification tool, and many shops own both for exactly that reason.
At 6.91 pounds it is meant to stand on a bench. If your layout work moves around a lot, that weight becomes an argument for the 6 inch version or a digital gauge instead.
5. Diydeg CNC 3D Finder Universal 3D Sensor Probe – Best for Circle Center Finding
CNC 3D Finder, Professional Universal 3D Sensor Probe, Multifunctional 3D Locator with Tungsten Steel Tip for X, Y and Z Axis, for for GRBL CNC
Locates in X, Y and Z
Under 0.01 mm specification
24V DC supply
USB-C cable, 6.6 foot
Pros
- X
- Y and Z locating in one probe
- Circle centre finding and table shape measurement built in
- Green and red LED shows power and trigger state
- Dustproof anodized housing with an anti-roll flat
- USB-C connection avoids a proprietary connector
Cons
- Some arrive with bent probe tips
- Accuracy reported by users at around plus or minus 0.004 inch
- M2.5 tip thread limits replacement options
- May need a cable extension depending on machine layout
Circle centre finding is the feature that separates this probe from the others. Most probes trigger when they touch; this one can be told to treat the workpiece as a shape, touch at several points around an edge or a hole, and report the centre of that circle back as a coordinate. That is real coordinate work rather than a touch event.
On paper the specification is strong. Measurement accuracy is quoted under 0.01 mm, the housing is anodized aluminum alloy with a flat anti-roll face, and the tip assembly is a stainless steel needle with a tungsten steel ball head. It runs on up to 24 volts of direct current and connects with a USB-C cable rather than a circular aviation plug.
There is an LED status light that reads green on power and red when triggered, which is more than many inexpensive probes offer and saves time when you are wiring the thing in the dark. Compatibility is reported as good with Centroid Acorn and MACH3, and the unit is specified for GRBL equipment.
Now the part reviewers actually complain about, which is worth more than the datasheet. Some owners report units arriving with bent tips, and the fix is to work on them with the adjustable set screws. Others report readings around plus or minus 0.004 inch, coarser than the 0.01 mm headline figure implies once you convert it – a real gap between specification and delivered performance on some units.
The M2.5 thread on the tip is the quiet limitation. When a ball tip wears, dulls or bends, finding a replacement is harder than it would be with a coarser thread, and that matters for a consumable part on a probe that gets used daily.
When it makes sense
Choose it when your work repeatedly involves finding the centre of an existing hole or the centre of a round feature – reaming, tapping, drilling into a located boss, or any job where centring errors get expensive. The circle centre routine removes the slow manual approach of touching two opposite sides and averaging.
The LED also makes it a good first probe for a shop learning to interface a probe at all, because you can see the trigger state without running a test program.
Where it falls short
With 25 ratings averaging 4.2 stars, this is the thinnest evidence base among the better-rated probes here. A 4.2 average on a small sample often means a good product with a small number of early units that had problems, and that is a real risk when the part is a consumable you will replace.
Inspect the tip the moment it arrives and before it touches a machined surface, because a bent tungsten ball will mark work and will not read true. The lack of an industrial connector option and the 6.6 foot cable are also worth checking against your machine layout before you commit.
6. YIDOFENG MF60 3D Touch Probe Edge Finder – Best for Standard M4 Machine Fit
YIDOFENG 3D Touch Probe Edge Finder for Metals, accuracy :0.01mm,M4 thread
X, Y and Z three-direction
M4 thread, 4 mm ball, 40 mm long
Under 0.01 mm accuracy
Metal-only detection
Pros
- M4 probe thread is a far more common standard than smaller alternatives
- Under 0.01 mm accuracy and repeatability both specified
- Trigger life rated at 5 million cycles
- Probe rotates 180 degrees for awkward approach angles
- Waterproof and dustproof with a green trigger light
Cons
- Only detects on conductive metals
- so it will not work on plastic or composite work
- Draws more power
- so a weak supply may not light the indicator
- Over-travel beyond plus or minus 6 degrees in XY or 1 mm in Z damages the probe
The thread is the headline here. A probe that screws in with a common M4 fitting will fit hardware many people already own, and when the ball tip eventually needs replacing you can source it. That single decision removes the most common reason a cheap probe becomes a paperweight.
Everything else is specified properly too. Accuracy and repeatability are both quoted under 0.01 mm, the ball head is 4 mm in diameter and 40 mm long, the probe direction is plus or minus X, plus or minus Y and plus Z, and the trigger life is rated at 5 million cycles. The body is an aluminum profile, 4.09 by 0.28 by 4.49 inches and 6.3 ounces, with a green light that comes on when the probe triggers.
Two details set it apart from the generic probes. The 180 degree probe rotation means you can approach a feature from a direction that suits the holder rather than one fixed angle, which removes a common cause of a mis-set probe. And the water and dust sealing matters in a shop where the probe is mounted permanently and gets coolant spray every job.
The metal-only limitation is a genuine constraint rather than a flaw. Detection relies on conductivity, so it works on steel, aluminium and brass and does nothing on plastic, composite or a non-conductive fixture. If you machine polymer parts, this is the wrong probe and you need a spring-style or optical alternative.
Power consumption is the other thing to plan around. Reviewers note the light may not come on if the supply is weak, and a probe that seems dead is much more often a supply problem than a failed probe. Match the machine supply to the 24 volt maximum before you start troubleshooting the wrong thing.
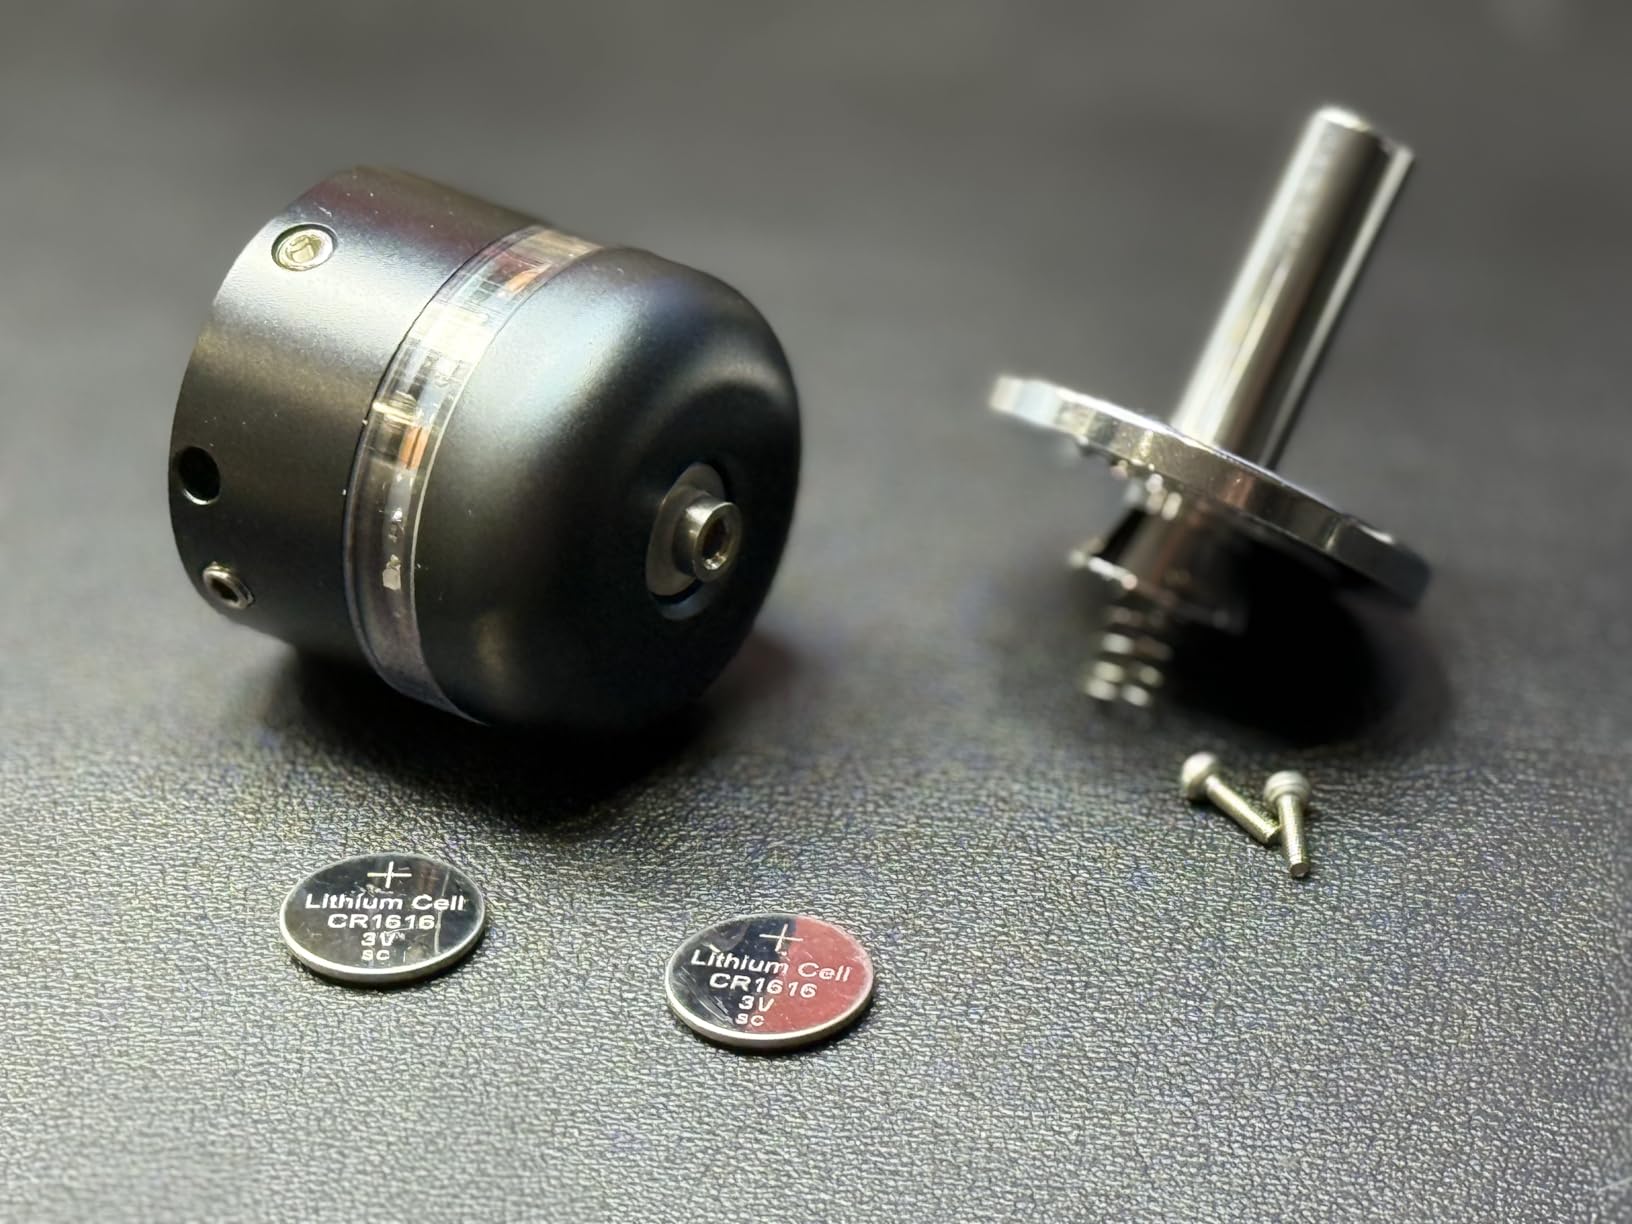
Owner photos of this probe are worth a look before you order, because the mounting end and the ball tip are the two places where copies differ. The photos show a compact body that clears a spindle nose without a long adapter stack, and a trigger light that stays easy to see once the machine is running.
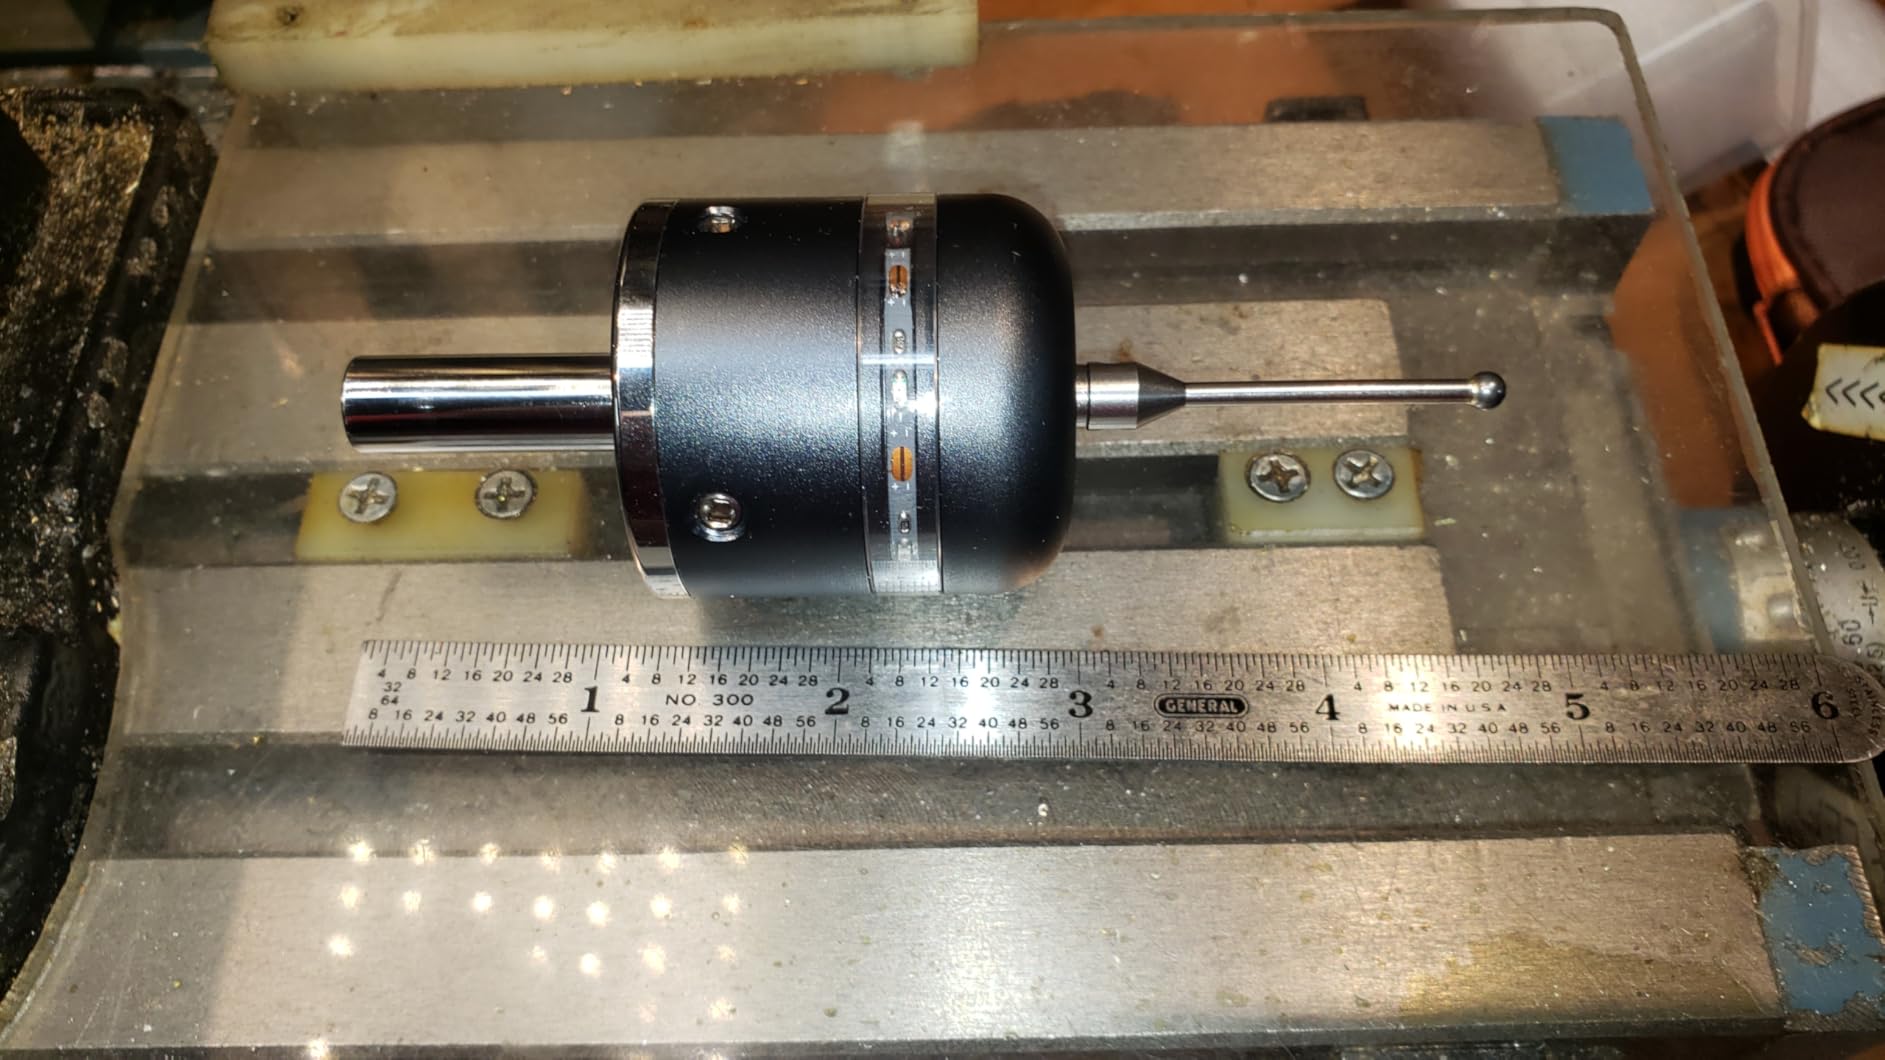
Several of the customer images focus on the 40 mm probe length, which is the dimension that decides whether it can reach into a deep pocket. If your pockets run deeper than the probe is long, this will not work in them and you need a longer version or a different tool entirely.
How to protect it in normal use
Set the software probe distance as short as your accuracy requirement allows, because the safety stroke is only plus or minus 6 degrees in XY and 1 mm in Z. Every millimetre of extra travel you permit is a millimetre of possible damage from an overshoot, a mistyped coordinate or a crash.
Keep the ball head clean and polished. A ball with swarf packed around it changes its effective trigger point, and the reading drifts with it. A soft brush and a drop of oil at the end of a shift is all the maintenance this needs.
Where it falls short
With 18 ratings at 4.1 stars this is the newest and least proven product in the roundup, and the review history simply is not there yet. There is also a single colour variant, so if you run more than one machine you may want identical probes rather than a mixed set.
The over-travel limit is strict enough that a beginner can damage it. If you are learning CNC probing on this machine, set conservative values and stay in manual until you trust the software. Buying a spare ball tip at the same time is cheaper than learning that lesson twice.
7. Starrett Electronic Height Gage 0-6 Inch – Best for Datum-Referenced Layout
Starrett Electronic Height Gage, 0-6″ Range, .0005″ Resolution
0-6 inch range
0.0005 inch resolution
Depth attachment included
Hardened stainless steel bar and base
Pros
- 0.0005 inch resolution on an electronic readout
- Depth attachment lets it read internal dimensions
- Auto-off after five minutes protects the coin cell
- Vertical bar set back from the nose for stability
- Protective case included and made in USA
Cons
- Only 6 inch of range
- which is short for large workpieces
- CR2 coin cell rather than standard AA or AAA batteries
- Weighs 3 pounds
- and the review base is small at 41 ratings
Starrett builds this one in the United States from a hardened stainless steel bar and a hardened, ground and lapped base, and the spec sheet calls out a detail that tells you the design was thought about rather than assembled: the vertical bar is set back from the nose edge. That setback is what keeps the gauge from tipping forward when the head carries a depth attachment out over a bore.
Resolution is 0.0005 inch on a clear LCD with characters 0.932 inch high, which is large enough to read while leaning over a bench. You get inch and millimetre switching, a thumb roll for fine movement of the head, and a depth attachment in the box, which is the piece that turns a height gauge into something that can check step depths and blind hole depths.
Auto-off after five minutes is a small quality-of-life decision that matters on a coin cell. The gauge is specified for one CR2 battery, included, and an electronic height gauge that empties itself while you are at the machine across the shop is a genuinely annoying failure mode.
The finger grooves in the base are a small thing that tells you it is meant to be held. Layout work means picking the gauge up, setting it down and picking it up again, and a base you can actually grip makes that less of a fumble.
Where it fits is narrow but real. At 6 inches it is a bench instrument for small parts, and if your largest workpieces are bigger than that you need the 12 inch gauge later in this guide. The honest limitation is that the review base is only 41 ratings, so the long-term ownership record is thin even though the brand history is long.
How to use the depth attachment properly
Slide the depth bar into the head, extend it past the jaw face, and zero on the outside of the workpiece before you go inside. Zeroing on the outside and reading inside is what keeps a step depth from absorbing the offset of the tool tip, and it is the single most common way depth readings go wrong.
Check the depth bar for bend before trusting it. A bar that has been dropped will read consistently but incorrectly, and no amount of care with the rest of the gauge will fix it.
Where it falls short
Six inches of range is the main constraint, and there is no way around it. Buying a 6 inch gauge and then needing 12 inches means owning two, so if you already know your largest workpiece, measure it first.
It also runs on a single CR2 coin cell rather than a standard battery, which is a recurring small annoyance across the height gauges in this roundup rather than a fault of this model. And at three pounds it is a tool you set down on a bench, not one you carry between a mill, a lathe and a grinder.
8. Mxmoonfree 12 Inch Digital Height Gauge – Best Feature Set for Layout and Presetting
Mxmoonfree 12″ (300mm) Digital Height Gauge 0.0005″/0.01mm Resolution
12 inch and 300 mm range
0.0005 inch and 0.01 mm resolution
Plus or minus 0.001 inch accuracy
Cast iron base, 8 mm indicator bracket
Pros
- 12 inch range with 0.0005 inch resolution in a digital readout
- Accuracy of plus or minus 0.001 inch verified by owners against gauge blocks
- Quenched cast iron base is stable where a folding base is not
- ABS and INC measurement modes plus inch and millimetre switching
- 8 mm bracket for a dial indicator and a data output port
- Hard-shell case and LR44 batteries included
Cons
- Display must be read close to square
- or readings shift
- The 8 mm indicator holder is described as a tight fit for some stems
- Only 16 ratings
- so long-term reliability is unproven
- Brand carries far less shop history than Starrett or Mitutoyo
This is the most capable bench gauge in the roundup on paper, and owners who have checked it report that the paper holds. The accuracy is specified at plus or minus 0.02 mm, which is 0.001 inch, and the review summary notes that users verify it with gauge blocks – the right test, and the one we would run ourselves.
Range is 12 inch or 300 mm with 0.0005 inch and 0.01 mm resolution, so the same gauge covers imperial and metric layouts without a second tool. It also offers absolute and incremental measurement modes, which sounds like a detail until you realise incremental mode lets you zero anywhere and carry that reference through the whole job.
The base is quenched cast iron and weighs the gauge up to 8.88 pounds, which is heavy on purpose. A cast base will not flex, so the reading reflects the part and not the gauge, and that is exactly what you need when you are using the tool to check a flatness claim or set a plane.
Two accessories make it more than a ruler with a jaw. The 8 mm bracket lets you mount a dial indicator on the head, which turns the gauge into a height-reading base for deviation work without a separate magnetic base. The data output port lets readings go to a computer or a spreadsheet, which is the closest thing to reporting in this whole roundup.
Fine micro-adjustment covers the weakness that hurt the cheaper digital gauge earlier in this guide. A micro wheel means you can bring the carriage onto a value slowly and lock it, which is the difference between a gauge you can set to a specific height and one you can only approach.
Where the extras pay off
Zero-setting at any point is the feature you will use every single time. Set the head on the table, zero, and then every reading afterwards is relative to that surface – which is precisely how a coordinate measurement is defined, as an offset from a datum rather than an absolute number.
The indicator bracket is what turns this into a presetting instrument. Put a test indicator in the holder, zero on the tool you have set, and the gauge becomes a readout of how far the next tool is from the first. That is the hand-tool version of a CNC tool presetter.
Where it falls short
The display viewing angle is the complaint to know about. It has to be read close to square to the face, and reading it from above at an angle gives a number that does not match what you get from straight on. On a bench where you are constantly leaning over, that is a real habit to build.
The 8 mm indicator holder is reported as a tight fit, so check your indicator stem before assuming a standard one will drop in. And with 16 ratings at 4.8 stars, the sample is small enough that a single batch problem would move the average – this is the highest-rated product here, not the most proven one.
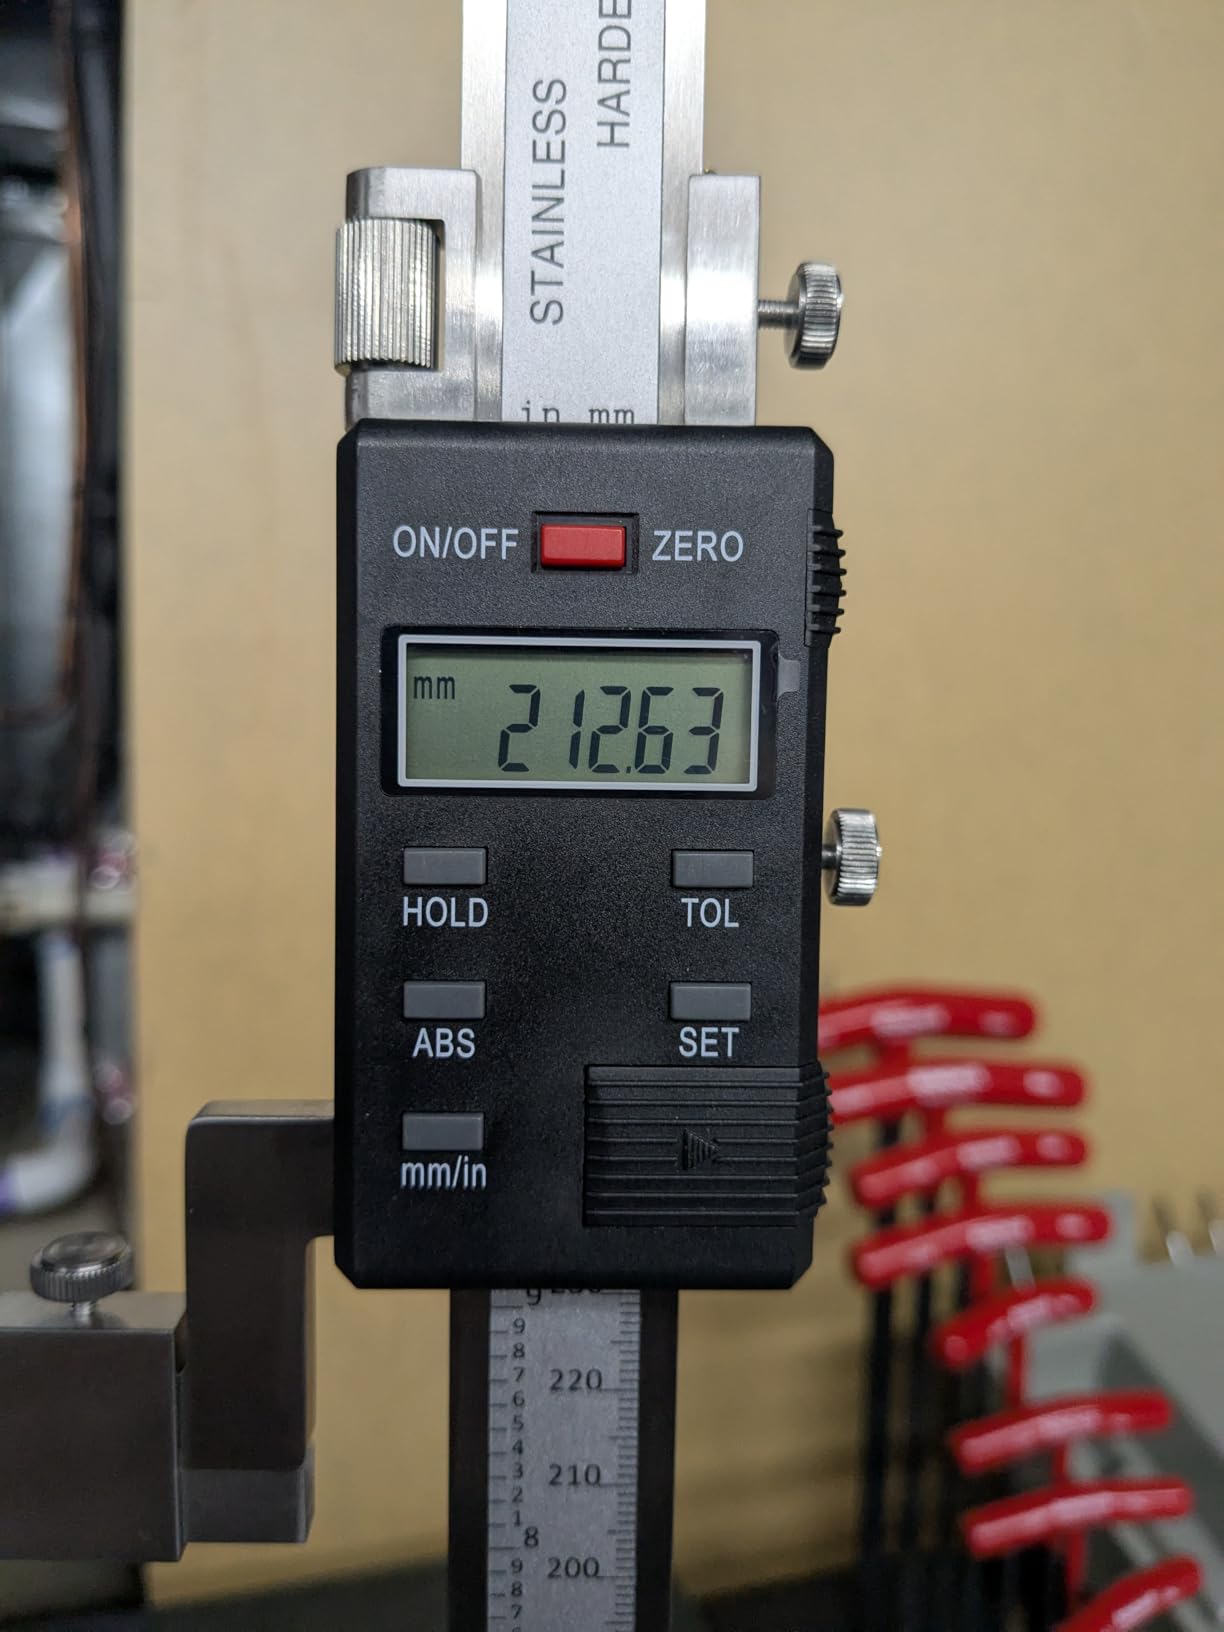
Customer photos of this gauge show the feature that justifies the cast iron weight: the base is a single rigid casting rather than a folding sheet-metal foot. Owners with the 12 inch version commonly photograph it on a surface plate, which is the correct place for it.
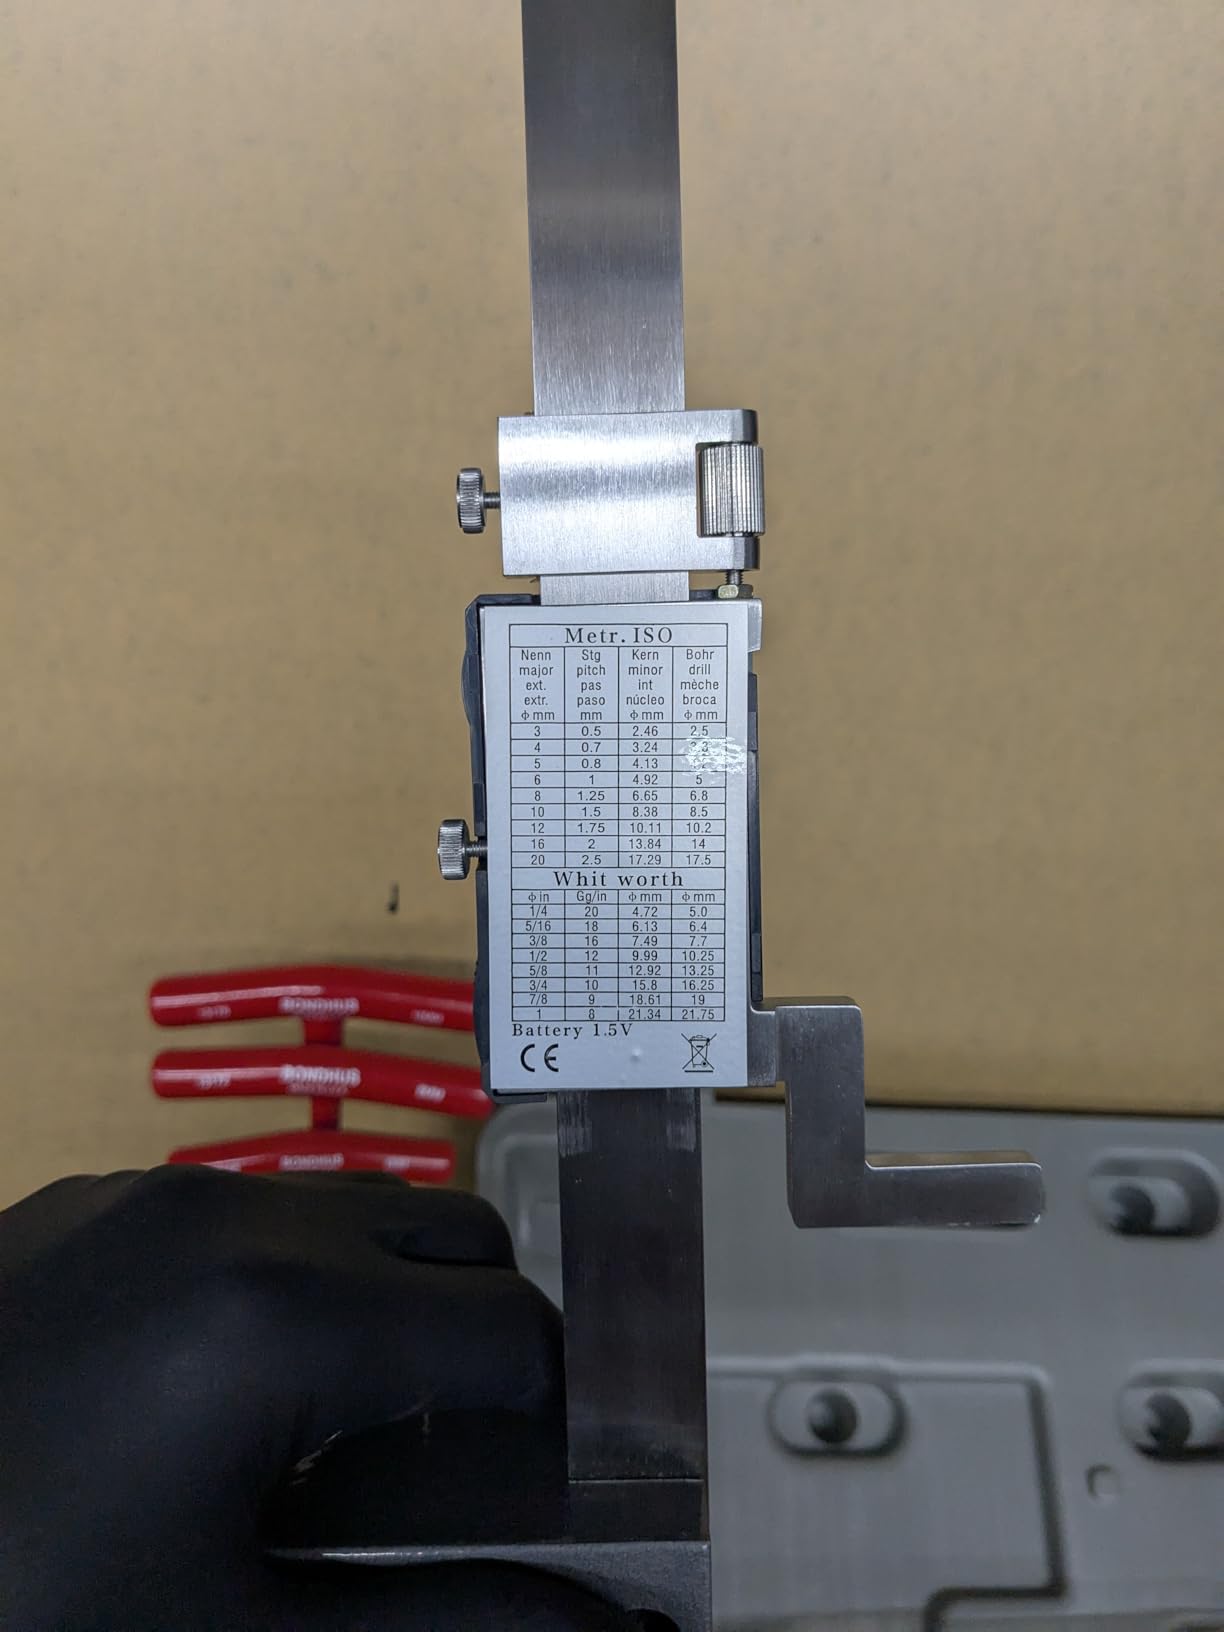
Other images focus on the head and the 8 mm indicator bracket, and they make the clearance obvious. A dial indicator fitted in that bracket clears a good range of part sizes, but the holder is snug, so plan to check your stem diameter rather than assume.
9. Starrett 827B Edge Finder – Best Accuracy for X and Y Centering
Starrett Edge Finder, .200″ Contact Diameter, .500″ Body Diameter
Double ended
Plus or minus 0.00012 inch accuracy
0.200 inch contact, 0.500 inch body
Hardened ground lapped tool steel
Pros
- Plus or minus 0.00012 inch accuracy
- the tightest stated figure in this roundup
- Double ended
- so one tool handles two standard sizes
- Hardened
- ground and lapped tool steel that stays true
- Locates edges
- centres
- scribed lines
- shoulders
- grooves and round work
- Protective case included with a 1 year limited warranty
Cons
- Costs more than a generic edge finder for a simple job
- Mechanical only
- with no electronic readout
- Reading the deflection by feel takes practice to do quickly
An edge finder answers one question with one method: when the tip stops deflecting, where is the edge? The cylindrical contact is a known diameter, so the moment it kicks, the spindle centre is exactly half that diameter past the edge. That is a coordinate in X or Y, derived from geometry rather than from a display, and it is repeatable to far better than most people expect.
This one is a double ended 827B with a 0.200 inch contact diameter and a 0.500 inch body diameter, hardened, ground and lapped tool steel, made in the USA with a one year limited warranty and a protective case. The stated accuracy is plus or minus 0.00012 inch, which is the finest figure of any tool in this roundup.
Double ended matters more than it sounds. One end is a standard contact and the other is a different size, so the same tool handles a 0.375 inch and a 0.500 inch body configuration without a second purchase, and the case keeps them from mixing on the bench.
The listed uses are exactly the coordinate tasks you would expect: flat edges, straight edges, shoulders, grooves, scribed lines and round work. A scribe line matters more than beginners expect, because marking a centre on a rough face with a straight edge gives you a repeatable starting point that eyeballing does not.
What you are actually doing is watching the deflection, not reading a number. The tool leans over as it touches, then kicks back when the contact is centred on the spindle axis. Reading that kick is a skill, and the owners who describe the smoothest operation are the ones who have done it a few hundred times.
How to centre a workpiece properly
Zero the machine or the knee at the centre of the contact diameter, then lower the edge finder until it just stops kicking and note the reading. The actual edge sits half the contact diameter to one side, so the centre of your workpiece is the reading plus or minus 0.100 inch for the 0.200 inch contact. Getting that sign right is the whole learning curve.
Do it in two axes, and always approach the same direction. The reading differs slightly depending on which way the deflection was taken up, so a consistent direction is what makes the number repeatable the second time you need it.
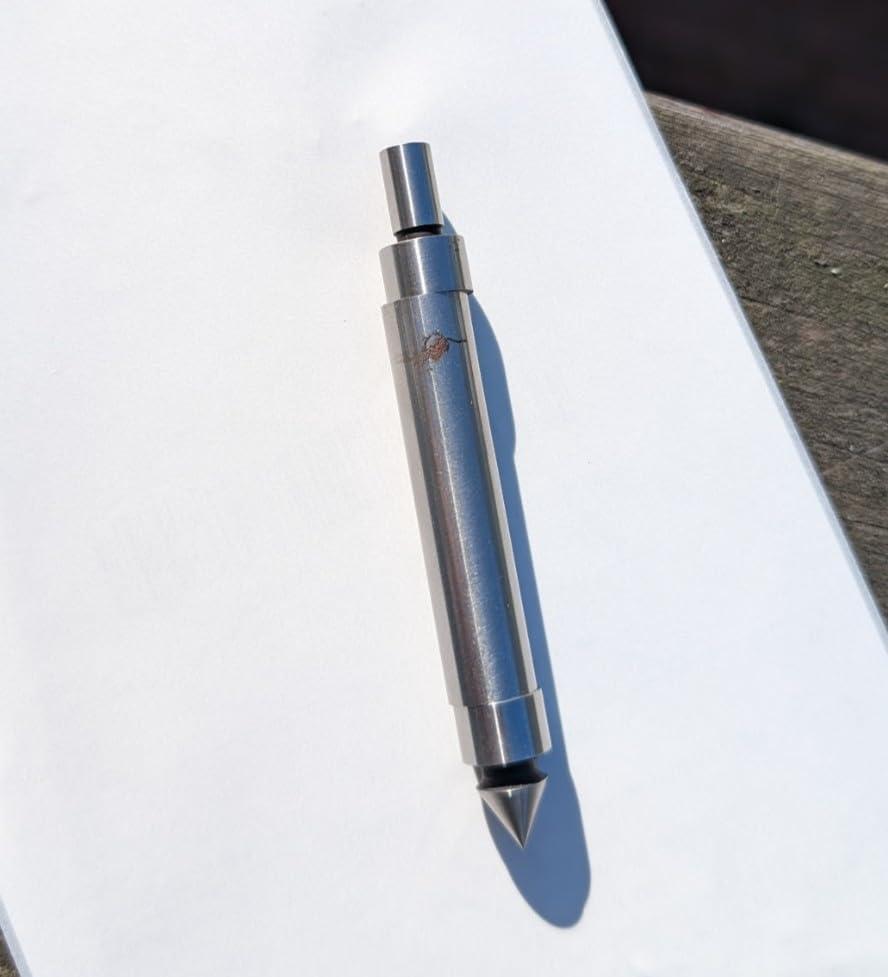
Customer photos of the 827B typically show it lying in its case next to the machine, and they make the case worth having visible. A ground and lapped edge finder with a 0.200 inch contact will pick up a chip or a ding in a week of normal use, and the case is what keeps that contact diameter true.
Where it falls short
It is an expensive edge finder, and for a lot of home work the cheaper one produces an edge location good enough for the tolerance in hand. If you are only ever centring a workpiece to within a few thousandths, the accuracy gap between plus or minus 0.00012 and plus or minus 0.0005 is smaller than your setup error.
It also has no readout. There is no screen, no data output, and no way to write the coordinate into a log except by hand. On a CNC that matters, because a probe reports the position automatically, and on a manual mill it matters less because you are moving the quill by hand anyway.
10. Brown and Sharpe Standard Edge Finder – Budget Pick for Everyday Centering
Brown & Sharpe Standard Edge Finder, Single-End Usability for Easy Setup
Single ended
Plus or minus 0.0005 inch
0.200 inch tip, 3/8 inch shank
Precision ground contact surfaces
Pros
- Plus or minus 0.0005 inch accuracy is plenty for most home shop tolerances
- 0.200 inch tip diameter on a 3/8 inch shank fits standard milling collets
- Precision ground contacts give a clean
- readable kick-off
- Hardened alloy steel at 22.68 grams
- 285 ratings make it one of the most proven picks here
Cons
- Single ended
- so a second size means a second tool
- Mechanical only
- with the same learning curve as any edge finder
- Basic design with no case
- readout or extra features
This is the edge finder most home machinists will actually end up with, and the reason is straightforward: it does the job at an accuracy most garage work never asks to beat. A 0.200 inch tip machined to plus or minus 0.0005 inch of nominal size centres a workpiece to a couple of thousandths, which is finer than the runout on a hobby mill spindle.
It is a single ended tool on a 3/8 inch shank, hardened alloy steel, made by Hexagon Metrology under the TESA Brown and Sharpe name. The shank diameter is the detail to check first, because 3/8 inch is a standard milling shank that fits common collet and holder sets, so it drops into an existing setup without a purchase.
Precision ground contact surfaces are what separate a usable edge finder from a bad one. The deflection has to be predictable enough that you can see when it changes from leaning to kicking, and a rough or elliptical contact gives an ambiguous signal that makes every reading a judgement call. Owners report smooth operation and a visible kick-off, which is exactly the behaviour you want.
With 285 ratings averaging 4.6 stars, this is one of the most proven products in the roundup, and that matters for a part this simple. A plain hardened steel cylinder has very little to fail, and the reviews describe exactly that: no complaints about electronics dying, because there are none.
The trade against the Starrett double ended version is simplicity for precision. You give up the second size and roughly four times the accuracy figure, and in exchange you get a lighter 22.68 gram tool, a simpler design, and a cost that makes it reasonable to own several so one lives in each machine.
When it is the right call
Buy this one if your tolerance work is at 0.005 inch or looser, which covers a very large share of home machine work: brackets, furniture joints, adapters, jigs and general layout. At that level the accuracy of the finder is not your limiting factor – the spindle runout is.
It is also the right tool for learning. A single-ended finder with one known contact diameter is the simplest version of the technique, and once you have read the kick reliably on it, a more accurate one will feel effortless.
Where it falls short
Single end is the obvious limitation. If you work with different collet or holder configurations, you will end up wanting the other end, which is exactly what the double ended design exists to solve.
It has no case in the listing, and an edge finder stored loose in a tool drawer is how contact diameters get damaged. Keep it somewhere padded, or buy one of the double ended tools that ships with a case, if your shop is rough on small precision parts.
How to Choose Coordinate Measuring Tools for a Home Shop
Start with accuracy, not resolution. The single most common mistake in home metrology is buying a tool with a long decimal on the display and assuming it is correct. Resolution is what the tool can show; accuracy is how close that number is to the truth. A probe quoting 0.01 mm repeatability is telling you how closely it returns to the same point, which is a different and equally valuable claim.
When a listing gives one number and no test method, treat it as unverified. The cheapest way to find out is to check a new tool against a known reference the day it arrives, and a single pass tells you more than any number printed on a box.
Decide mechanical or electronic once. Mechanical tools – dial height gauges, edge finders, dial indicators – never fail because a battery died, and they give a continuous reading you can watch. Electronic tools give a direct number, support unit conversion, and can output data, but they carry electronics, coin cell batteries and firmware that will eventually disappoint you.
There is no wrong answer here. Plenty of working shops own both types of the same tool for exactly that reason, and if you can only fund one, the electronic version is easier to learn and the mechanical one is easier to trust for a decade.
Match the probe to your control, not to your ambition. This is where hobby probing goes wrong. A three-axis probe is only as good as the software interpreting it, so confirm that your controller lists the probe and that your breakout board has the probe input it needs before you buy hardware. The PGFUN unit here names GRBL, MACH3, Mach4, LinuxCNC, UCCNC and Centroid, which covers most setups people actually own.
On a manual mill, none of that applies. An edge finder plus a height gauge covers the same ground with no electronics, no wiring and nothing to go wrong, and it is why four of the ten tools in this guide are manual.
Check the thread and shank standard before anything else. Probe thread size determines whether you can fit a replacement tip, and shank diameter determines whether the tool fits your holder. M4 appears on the YIDOFENG probe and is a far more common standard than the M2.5 thread reported as a limitation on the Diydeg unit. The 3/8 inch shank on the Brown and Sharpe finder fits standard milling collets; a non-standard shank means buying a holder before you can use the tool.
Starrett and the premium brands versus the budget brands, in one sentence. The premium names are not automatically more accurate, but they are more consistent, better supported with replacement parts, and more likely to hold their published specification over years of use – and where the budget tools are thin is exactly the fit and finish that makes a measurement repeatable.
Forum experience bears this out. Practitioners consistently report that accuracy rather than resolution is the real differentiator, and that budget brands overstate accuracy on paper. The counter-argument is equally well sourced: some older production lines from established makers now measure less accurately than they used to, because manufacturing has moved. Judge the model, not the badge.
Think about the whole setup, not the individual tool. A 12 inch height gauge on a warped piece of MDF measures the warp. Every tool in this roundup is only as good as the surface it is standing on, so budget for a surface that is flat, stiff, clean and big enough – and keep it that way. A home shop with a good datum and a modest height gauge will beat a home shop with premium tools and no reference surface.
Buy one of each group before you buy a second of any. The most common purchasing error is owning three calipers and nothing to put them on. Get the XY answer, the Z answer and a reference, then decide where the gaps are. If you cannot see what a tool is measuring, it will sit in a drawer.
We do not think a calibration certificate is a buying requirement at this level. Verification against a known standard on arrival tells you more about that particular tool in your particular shop than a certificate does, and it is the habit that will keep you honest for years afterwards.
Building a Home Shop Coordinate Measurement Workflow
A coordinate measurement setup is a chain, and every link has to be traceable to a datum. Here is the order that works, and it is worth walking through once so each step means something when you reach it.
1. Establish the datum. Before any measurement, decide what the part is measured from. A surface plate or a well-supported machine table is the datum. Clean it, check it is not warped by putting a straightedge across it, and keep one location on the machine as your reference for every job. Measuring from a different corner on each setup is what makes numbers irreproducible.
2. Find X and Y with an edge finder. Lower the finder until it just stops kicking, note the reading, and add or subtract half the contact diameter. Do it in both axes, always approaching the same way. For a CNC machine, run the equivalent routine with a three-axis probe and the machine records the coordinate instead of you writing it down.
3. Fix the Z coordinate with a height gauge. For layout, stand the height gauge on the datum, zero, and read or scribe. For CNC, the tool setting probe reports the Z offset to the controller and it stays there. Either way the number is relative to the datum, not to the room.
4. Take the dimension with a hand tool. The edge finder and height gauge find and read a coordinate; a caliper or micrometer measures the size of a feature once you have found it. These are different jobs and beginners routinely try to do both with the same tool, then wonder why the tolerance does not hold.
5. Check deviation and alignment. For runout, flatness, parallelism and perpendicularity, mount a dial test indicator on a magnetic base and swing it through an arc against the datum. This is the step that catches a spindle that is out of true or a vise that is not square, and it is the job a CMM does better than any hand tool because it holds a stylus on a known point.
6. Record it. This is the step most home shops skip and the only one a CMM cannot skip. Write down the readings, the tool used and the date in a notebook. When a part starts failing on the third one, the log tells you whether the tool drifted or the process did.
Tramming a mill is the same chain applied to the machine. Use a test indicator against the table to check the head over its travel, adjust until the sweep is inside your tolerance, and you have not just fixed the mill – you have built your first measurement setup and learned to use it.
For anyone who enjoys watching other people solve this, hobby-built and DIY CMM projects built from router kits, cameras and existing DRO hardware have genuine momentum in the machining communities, and the probes in this roundup are the sensing half of exactly that idea.
Care, Calibration, and Common Mistakes
Clean the ball tip, and do it often. A tungsten ball with swarf packed around it changes its effective diameter and its trigger point, and every reading drifts with it. A soft brush and a drop of light oil at the end of a shift is all the maintenance a touch probe needs.
Respect the over-travel limits. The safe stroke on these probes is small – plus or minus 6 degrees in XY and 1 mm in Z on the YIDOFENG, for example. Exceeding it does not cause a reading error, it causes a broken probe. Set your software travel as tight as your accuracy requirement allows and stay in manual until you trust it.
Never measure on a part you are clamping. This is the classic beginner error. A caliper reading taken on a part still gripped in a vise tells you about the vise, not the part. Take the measurement off the machine, or loosen and re-clamp with a different reference. This applies to height gauges too, and the reason one is quoted as reading to a workpiece just off the machine.
Do not tighten a probe trigger by force. Trigger force is a specification, not something to overcome. Forcing the ball past its stroke or pushing a height gauge head down hard to get a number rocks the part and gives a reading that moves every time you repeat it. Close gently until the light comes on, then stop.
Keep a spare ball tip and a spare battery. Both are consumables. A bent or worn ball changes every reading that follows, and it is a five-minute swap if you have the part. The same applies to the CR2 and LR44 cells used across the height gauges here – keep a spare set with the tool, not in a kitchen drawer.
Verify on arrival, and then verify periodically. Run a new probe through its full travel against a known flat, and check a new height gauge against a known reference at a few points on the scale. Write the date down. A tool that reads correctly at the start of its life and drifts later is a solvable problem; one that was wrong from day one is a mystery.
Store small precision parts in their cases. A ground and lapped edge finder dropped in a drawer develops a contact diameter that is still within a couple of thousandths and no longer reads true. The cases included with the Starrett tools in this roundup are not packaging – they are the storage solution.
One last habit worth building early: write the measurement down. A CMM produces a report, a home shop produces a scrap of paper, and the difference shows up the day you need to prove a part was good before you cut three more.
Frequently Asked Questions
How much does a CMM cost?
Shop-scale coordinate measuring machines start in the tens of thousands of dollars and climb well past that with a probe, software and a controlled room, which is why they sit in businesses rather than garages. A home shop gets most of the same measurement discipline from a height gauge, an edge finder and a touch probe, and spends a small fraction of that. Budget for a flat reference surface first, because every one of those tools reads against it.
What are the different types of coordinate measuring machines?
The main types are bridge CMMs, which carry a probe on a moving bridge, gantry or bridge-style structures that move the probe along two rails, and vision measuring machines, which use a camera and software to read a whole part at once without touching it. All of them locate features in X, Y and Z, capture their size and shape, and report deviations against a nominal model.
Which measuring tool is the most precise?
A coordinate measuring machine is the most precise, but it is out of reach for a home shop. Among hand tools, a micrometer resolves 0.0001 inch, a dial test indicator reads to 0.0001 inch for deviation work, and a good electronic height gauge works at 0.0005 inch resolution. In this roundup the Starrett 827B edge finder carries the tightest stated figure at plus or minus 0.00012 inch.
Is a caliper or micrometer more accurate?
A micrometer is more accurate. A digital caliper typically resolves 0.001 inch, while a good outside micrometer resolves 0.0001 inch – ten times finer – and holds that accuracy better along its scale. A caliper is still the right first tool because it covers more size range instantly and reads internal and depth dimensions too.
What size height gauge should a home machinist buy?
Six inches covers small parts, tooling and most fixture work, and it is the size the Starrett electronic gauge in this roundup uses. Twelve inches, like the Shars dial gauge and the Mxmoonfree digital gauge here, is the better buy if you lay out plates, castings or anything over six inches. Measure your largest workpiece before you decide, because a short gauge will not grow.
Do I need a surface plate for my home shop?
Not to start. Most home work is measured against a machine table or a piece of known-flat material, and that is often good enough. You need a proper surface plate when you start checking flatness, parallelism or runout, or when you want height gauge readings that do not include the deflection of the thing you are standing on. It is the last purchase most shops should make, not the first.
Is Starrett as good as Mitutoyo?
Both are among the best makers of precision measuring tools, and for a home shop the honest answer is that a well-maintained Starrett is closer to a well-maintained Mitutoyo than their price difference suggests. Starrett is made in the USA with a long production history, while Mitutoyo is the larger manufacturer with more model options. Judge the specific model and its verified accuracy, not the badge.
What is a caliper measuring tool called?
A caliper is a two-jawed sliding measuring tool that reads outside dimensions, inside bores and depth from the same body. Digital calipers show the reading on an LCD and are the default choice for machinists, vernier calipers use a sliding scale with no batteries, and dial calipers use a mechanical dial for a continuous reading. For coordinate work the caliper takes the dimension, while an edge finder or touch probe finds the position.
Should I buy used measuring tools?
Yes, and the two edge finders in this roundup are the easiest place to start because a ground steel cylinder has little to fail. Buy a tool with its original case, check the contact surfaces or the ball tip for damage, and verify accuracy on arrival against a known reference before you rely on it. Avoid heavily used digital electronics where the display or the battery is already failing.
What is the best first coordinate measuring tool to buy?
A 6 inch digital caliper is the most useful first purchase for general measurement, followed by a 0-1 inch outside micrometer. If your work is specifically coordinate work on a mill, buy a height gauge next, because it is the tool that reads a Z coordinate. An edge finder is the cheapest way to add a repeatable X and Y location to a manual mill, and it pairs with the height gauge for almost nothing extra.
Conclusion
Pick by function, not by brand. The SainSmart Z-axis tool setting probe is our first choice because it removes the paper method from CNC work on day one and has the widest ownership record of anything here at 1152 ratings. The Starrett 827B edge finder is the manual answer for X and Y location and carries the tightest accuracy figure in the roundup, and the Brown and Sharpe single-ended finder is the same job at a fraction of the specification, which is plenty for most garage tolerances.
For a shop that has none of this yet, the order is a caliper, a 0-1 inch micrometer, a height gauge, an edge finder, then a dial test indicator on a magnetic base. For a CNC shop, add a three-axis touch probe – the PGFUN unit if your control software is listed in the manual and you have the breakout board for it, the YIDOFENG if a common M4 thread and replacement tips matter more to you than anything else.
Whichever route you take, build the chain: a clean datum, a repeatable XY location, a Z reading, a size, and a written record. That is the whole job, and these are the best coordinate measuring tools for home machinists because each one covers one link of it honestly. Verify any new tool against a known reference the day it arrives, keep a spare ball tip and a spare battery with it, and the set will still be telling you the truth in five years.
It is the same discipline we apply to a listening setup, and we wrote about that in our [amplifier guide for home](https://www.theclassicalshop.net/best-amplifiers-for-home/) – measure the thing properly once, then trust the number. For shop background audio while you work, our [soundbar picks](https://www.theclassicalshop.net/best-soundbars-for-home/) cover the same idea from the other end of the bench.